

Hot Rolled vs. Cold Rolled Cast in Channels: Key Differences, Benefits, and Applications
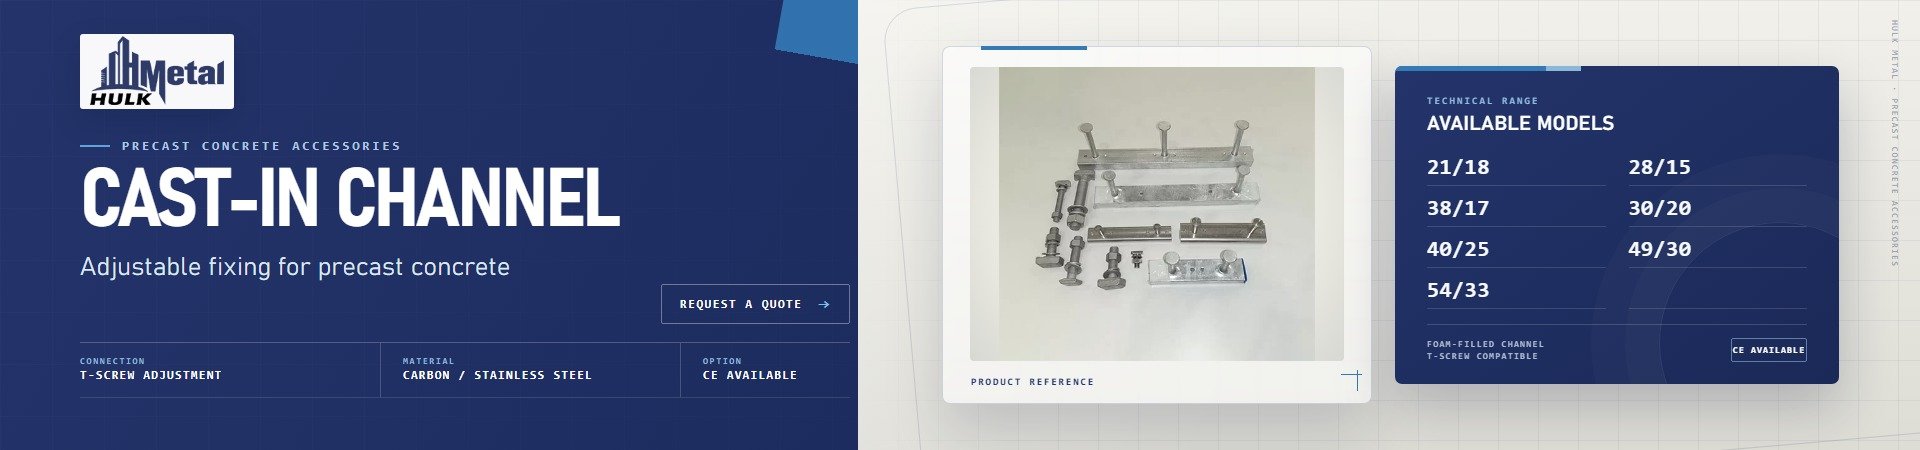
Cast-in channels are embedded in concrete to create reliable, adjustable fixing points for mechanical services, curtain walls, precast components, and structural connections. Because the channel becomes part of the finished structure, its profile, material, anchors, and installation method must be considered together. Hot rolled and cold rolled cast in channels use different forming routes, influencing dimensional control, surface condition, material behavior, and production economics. Neither process is automatically superior. Selection depends on the design load, approved system, section geometry, tolerances, environment, and order volume.
What Are Hot Rolled Cast in Channels?
Hot rolled cast in channels begin with steel that is heated above its recrystallization temperature and passed through a series of rolls until the required profile is formed. In a finished channel system, the rolled profile is then cut to length, punched or drilled as required, fitted with anchors, and prepared for surface protection.
Manufacturing and key characteristics
The hot rolling process can produce relatively substantial sections with stable overall geometry. It is commonly associated with thicker walls and heavier profiles, although actual dimensions and tolerances remain product-specific. Temperature, roll alignment, reduction schedules, straightening, and cooling must be controlled to maintain the intended section shape.
Hot rolled profiles may carry mill scale and require cleaning or descaling before coating. Surface preparation is therefore important when galvanizing or painting is specified. Mechanical properties should be confirmed from the steel grade, mill certificates, and product test documentation rather than inferred from the forming method.
Advantages and limitations
Hot rolled channels can be suitable where a robust profile, relatively thick material, or a particular heavy section is needed. The process can also support larger structural profiles. However, it involves significant heating and rolling equipment, and commercial availability may depend on standard roll sizes and production volume. Dimensional accuracy, straightness, and surface condition must still be inspected against the purchase specification.
What Are Cold Rolled Cast in Channels?
Cold rolled, or cold formed, cast in channels are produced from steel strip at or near room temperature. The strip passes through a sequence of driven rolls that progressively bends it into the channel profile. The formed profile is then cut, perforated, fitted with anchors, and coated where required.
Manufacturing and key characteristics
Cold roll forming is well suited to repeatable, high-volume production of thin-walled channels. Tooling can create comparatively complex edge details and slot geometry, and material utilization can be efficient. However, springback, roll wear, strip thickness variation, and residual stresses must be managed to maintain the intended dimensions.
Cold working changes the condition of the steel and may produce strain hardening. This does not mean that every cold rolled channel is stronger or weaker than a hot rolled alternative. Its mechanical behavior depends on the base steel, forming reduction, section geometry, and completed product design. Ductility, local buckling, and connection performance should therefore be verified from relevant calculations and testing.
Advantages and limitations
Cold rolled channels can offer efficient production, smooth surfaces, flexible profile design, and dimensional repeatability. These characteristics are valuable for standardized building services and facade systems. The main limitations relate to forming capacity, thin-wall behavior, residual stress, and local buckling. Any claim of suitability for a given load must be supported by the complete system, not by the manufacturing label alone.
Hot Rolled vs. Cold Rolled Cast in Channels: Key Differences
| Comparison factor | Hot rolled channels | Cold rolled channels |
|---|---|---|
| Forming temperature | Above the steel's recrystallization temperature | At or near room temperature |
| Typical section | Often relatively thick or heavy | Flexible thin-walled and complex profiles |
| Dimensional control | Depends on rolls, straightening, and finishing | Usually repeatable, with springback and tool wear controlled |
| Surface condition | May require removal of mill scale | Generally smoother, but may carry forming oils or residues |
| Material condition | Formed at high temperature | May develop work hardening |
| Production economics | Influenced by section size and rolling volume | Often efficient for standardized high-volume output |
| Typical selection basis | Heavier profiles where technically suitable | Standardized support, facade, and precast systems |
Mechanical properties
Hot rolling generally produces a relatively uniform wrought structure, while cold forming introduces deformation and residual stress. A direct comparison still requires the same base grade and a valid section and system design. Yield strength, elongation, effective section properties, weld details, and anchor behavior all affect performance.
Dimensional accuracy and surface quality
Cold roll forming can provide consistent slot dimensions and smooth surfaces in high-volume production, but thin material is sensitive to springback and handling damage. Hot rolled sections may have different dimensional ranges and surface conditions. For both products, the inspection plan should define permitted variation in width, height, wall thickness, slot opening, twist, camber, and length.
Production cost and efficiency
Hot rolled production involves heating and rolling, making section size and run length important cost factors. Cold roll forming requires dedicated tooling but can be efficient for repeatable thin-gauge products. Purchasing decisions should compare the complete installed cost, including anchors, accessories, coating, inspection, packing, freight, and installation time.
How the Manufacturing Process Affects Performance
Load-bearing capacity
Capacity is determined principally by the steel grade, effective cross-section, wall thickness, anchor design, weld quality, and concrete conditions. A heavy-looking profile is not necessarily stronger if its anchors or slot geometry are unsuitable. Design values must correspond to the tested direction of loading, concrete strength, edge distance, spacing, and any restrictions in the product approval.
Resistance to deformation
Hot rolled sections can offer stable, substantial geometry, while cold formed sections can be vulnerable to local buckling when thin walls are used under compression or bending. Well-designed cold rolled channels manage this through edge stiffeners, controlled thickness, and suitable fastener bearing areas. Installation damage and overtightening can also affect deformation and should be controlled on site.
Corrosion protection
Both hot rolled and cold rolled channels can be electro-galvanized, hot-dip galvanized, painted, or supplied in suitable stainless steel where specified. Performance depends on coating type, thickness, adhesion, coverage at edges, and exposure conditions. Hot rolled mill scale and cold rolling residues must be removed where they would interfere with coating quality.
Concrete anchorage and installation
Anchor shape, weld quality, embedment depth, and concrete confinement are critical. The channel opening must also match the specified T-bolt or accessory, and the filler strip must prevent concrete ingress during casting. Correct template fixing, concrete compaction, and controlled removal of the filler strip support reliable installation. Mixing components from different systems can invalidate assumed performance.
Applications of Hot Rolled and Cold Rolled Cast in Channels
Hot rolled cast in channels are often considered for heavy-duty precast connections, substantial structural interfaces, and projects requiring thicker profiles, subject to system verification.
Cold rolled cast in channels are widely used in precast wall panels, curtain wall brackets, pipe supports, cable trays, mechanical equipment, and other medium-duty building services. Their consistent slot geometry and efficient production make them suitable for standardized connections and repetitive installation.
Project matching begins with the design load and concrete details, followed by section dimensions, steel grade, anchors, accessories, coating, tolerances, and installation method. Approved load tables and project requirements take priority over assumptions about the manufacturing route.
How to Choose the Right Cast in Channel
Start with the design actions, including tension, shear, bending, dynamic effects, and load combinations. Confirm the proposed channel system is qualified for the actual concrete strength, cracked or uncracked condition, edge distance, spacing, and member thickness. Check the slot width and length against the specified T-bolt and fixing position. Select the steel grade and wall thickness from the approved design, not from visual appearance.
Next, define dimensional tolerances, coating class, anchor configuration, and required documentation. The buyer should request drawings, material certificates, dimensional inspection records, coating reports, and applicable load or system test evidence. For international projects, verify compliance with the governing local code and project specification rather than relying on a generic standard reference.
Quality Control and Testing
Effective quality control begins with raw material traceability. Steel grade, heat number, dimensions, and mechanical properties should be checked against the purchase order. Incoming strip or plate must also be examined for harmful surface defects.
During production, channel width, height, wall thickness, slot opening, hole position, length, straightness, and twist should be measured at defined frequencies. Anchor spacing and weld size require particular attention because these details transfer load into concrete. Where required, visual inspection should be supplemented by mechanical or non-destructive checks.
Before coating, surfaces must be cleaned according to the approved process. Afterward, inspect thickness, adhesion, coverage at cut edges, and freedom from bare spots. Packaging should protect the slot and coating, while records should link finished products to material batches and inspection results.
Why Choose HULK Metal?
HULK Metal supports custom cast in channel projects based on drawings, dimensions, steel grades, quantities, and coating requirements. Production planning can be aligned with the required profile, anchor arrangement, hole pattern, and delivery schedule. We coordinate material selection, forming, fabrication, surface treatment, inspection, and packing.
For each inquiry, providing the application, target loads, concrete conditions, coating standard, destination, and required documentation allows our team to evaluate feasible manufacturing options. Final product performance should always be verified against the applicable design and approval requirements for the project.
Hot rolled and cold rolled cast in channels differ in forming temperature, section capability, dimensional behavior, surface condition, and production economics. Hot rolled profiles may suit substantial heavy-duty applications, while cold rolled profiles offer efficient, consistent solutions for many precast and building services systems. The decisive factor is not the process name, but whether the complete product meets the project's structural, durability, installation, and compliance requirements.
Looking for reliable hot rolled or cold rolled cast in channels for your construction projects? Contact HULK Metal with technical specifications, and order quantities. Our team can help evaluate manufacturing options and develop a suitable production solution.
Article Navigation
PRECAST CONCRETE ACCESSORIES
OTHER RELATED ARTICLE
- 1.How to Choose High-Quality Shuttering Magnetic Products and Suppliers Guide
- 2.Applications and advantages of swivel hoist rings: HULK Metal provides you with safer and more flexible lifting solutions
- 3.Lifting Clutch VS Lifting Ring Clutch:Definition, Working Principle, Application Scenarios, and Selection Guide
- 4.Lifting Anchors: An Essential Component in Construction and Heavy Lifting
Other Precast Concrete Accessories You Might Want to Know
You can click to learn more about HULK Metal precast concrete accessories such as lifting anchors, precast sockets, spread anchors, shuttering magnets, cast-in channels, wire loop boxes, and other precast concrete accessories you might want to know.